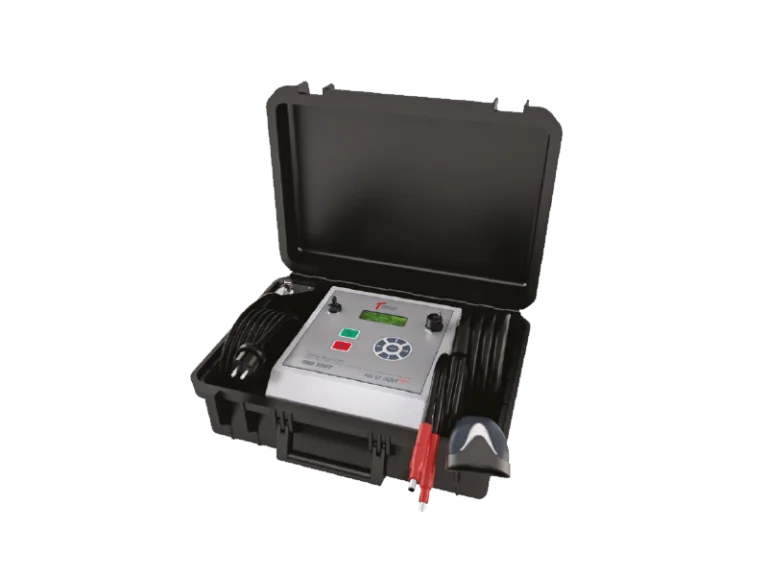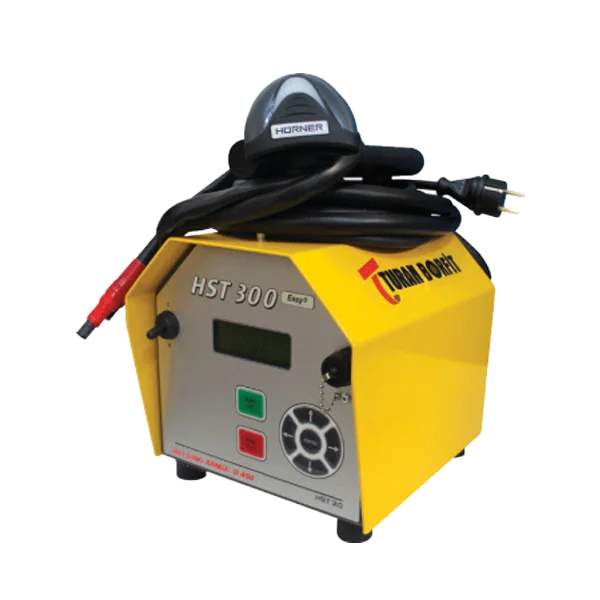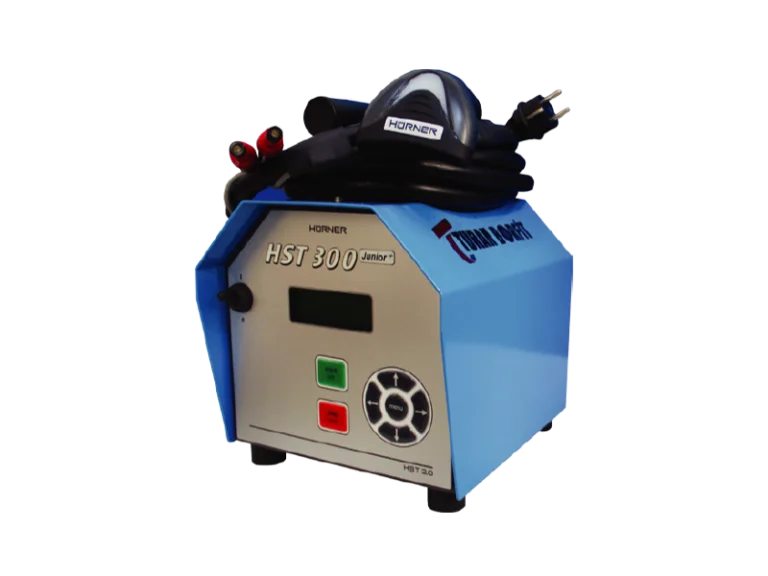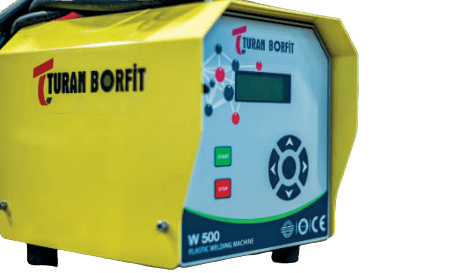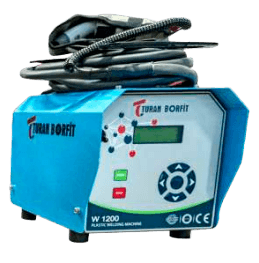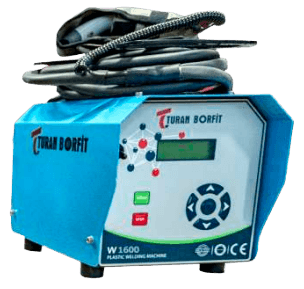
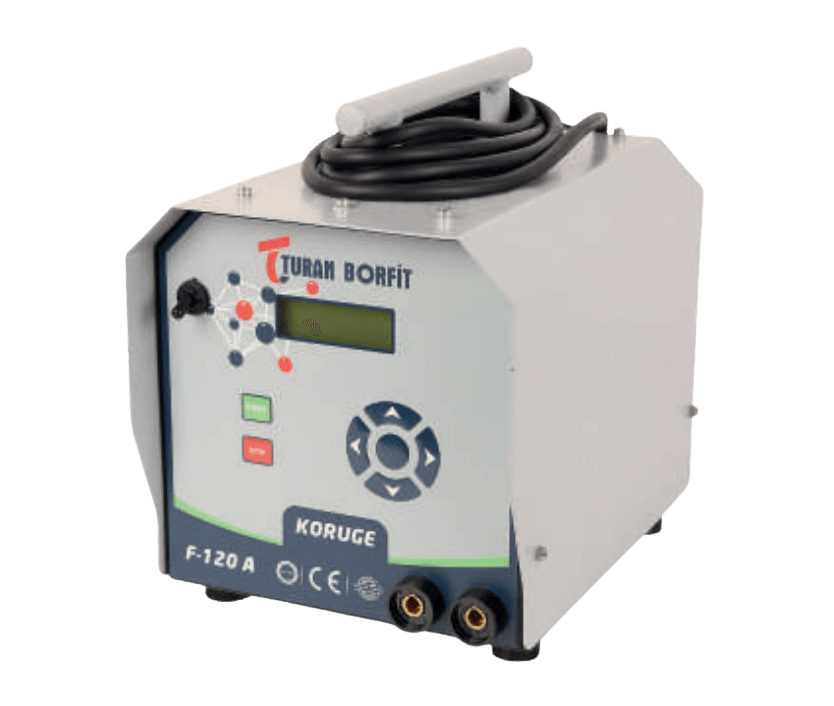
EF 120 A
Electrofusion Welding Machine
Electrofusion control units for PE, PP and PVDF fittings, with barcode input and weld logging.
Technical Data
Input
Single Phase, 50-60 Hz
Nominal Output Voltage
50 V DC
Output Current
100 A
Control
Microprocessor Controlled
Display
5x20 LCD Panel
Isolation Voltage
1500 V
Working Temperature
0 / +50 °C
Protection Class
IP 21
Microprocessor-controlled electrofusion welding machine with thyristor module control. Features a 5x20 LCD panel and delivers 50 V DC / 100 A output for precise PE pipe welding.
- Electronic Over Current Protection
- Adjustable Voltage, Current, and Time
- Natural Air Cooling
Visibility
Butt welds are visible and can be redone on the spot; EF welds hide inside the socket and need experienced welders.
Hard to reach places
EF wins: tiny machine, cable tip electrodes. Works above ground, in pits, anywhere.
Simplicity
Butt welding forgives workmanship errors; EF has zero tolerance and fails only at pressure test.
Material conditions
EF demands matching MFI, round pipes, clean surfaces, stable voltage; butt is unaffected by these.
Cost
Butt is far cheaper: no copper wire sockets every 6/12 m.
Strength
A correct butt weld is the strongest point of the line (the 'lip' adds wall thickness).
- Scrape the pipe surface in a thin layer; wipe with alcohol.
- Mark the pipe end at the coupler depth.
- Slide the coupler on with a snug fit.
- Connect the welding cables to the coupler.
- Scan the coupler barcode with the machine electrode.
- Press START at 'Ready to Weld'; wait until the machine cuts the current.
- MFI (melt flow) values of joined pieces must be close.
- Remove ovality with a clamping tool before welding.
- Always scrape the oxidized surface layer. It is the most neglected step.
- Pieces must interlock tightly (light hammer taps) without damaging the coil.
- Keep supply voltage stable at 210 – 230 V.
- If power is cut during welding, restart with a NEW coupler.
| Vehicle | L × W × H (m) | Volume | Max Load |
|---|---|---|---|
| 20 FT Container | 5.89 × 2.34 × 2.37 | 33 m³ | 24,850 kg |
| 40 FT Container | 11.90 × 2.34 × 2.38 | 67 m³ | 28,800 kg |
| 40 FT High Cube | 11.90 × 2.34 × 2.67 | 76 m³ | 30,200 kg |
| 45 FT High Cube | 13.00 × 2.34 × 2.67 | 86 m³ | 27,820 kg |
| Normal TIR | 13.6 × 2.45 | 100 m³ | — |
| Maxima TIR | 13.6 × 2.45 | 112 m³ | — |
| Jumbo TIR | 13.6 × 2.45 | 97 m³ | — |
| Truck + Trailer | 7.5 + 9.6 | 56 m³ | — |
Potable water lines, force mains, drainage and siphonic systems, natural gas distribution, agricultural irrigation and industrial pipelines. Fittings manufactured to TS EN 1555-3:2010+A1 • TS EN 12201-3+A1 • TS EN 15494 • CE; machines to TS ISO 12176-1 and DVS 2207 welding practice.
Catalogs, user manuals and training videos are available on request.
Request Documents