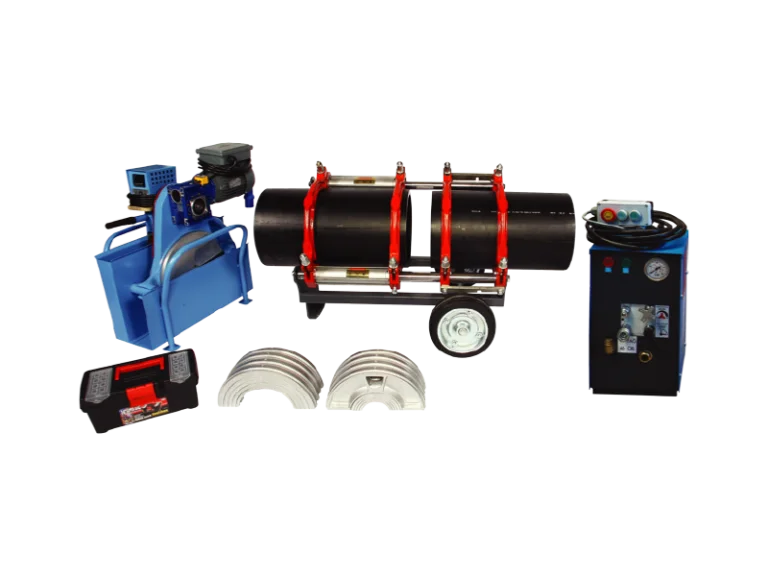
ALW 1000A
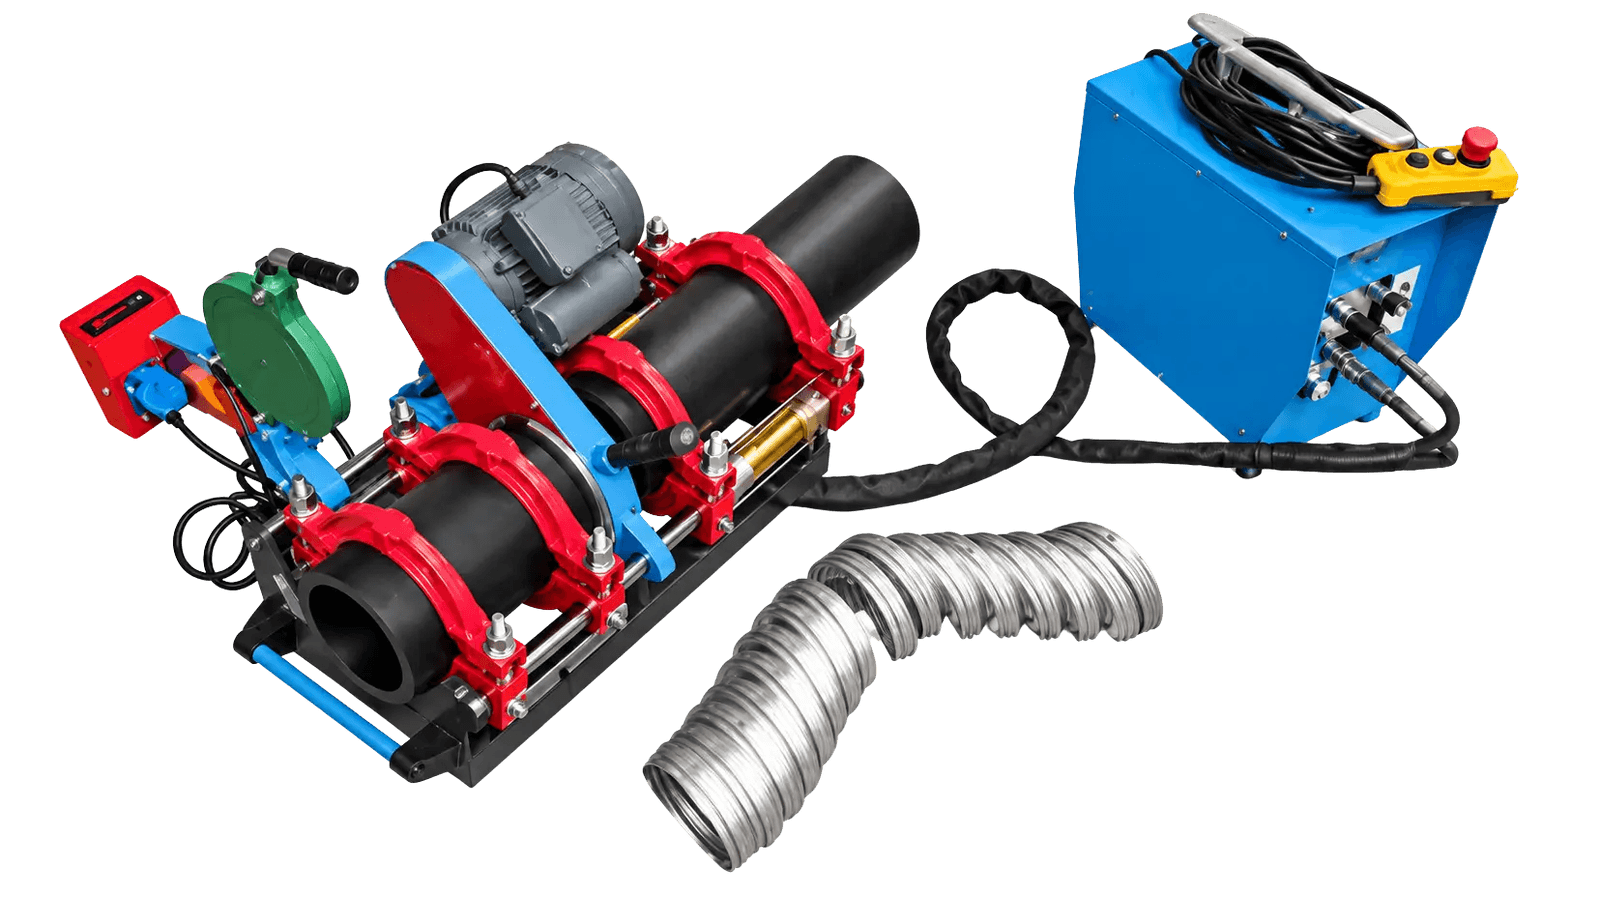
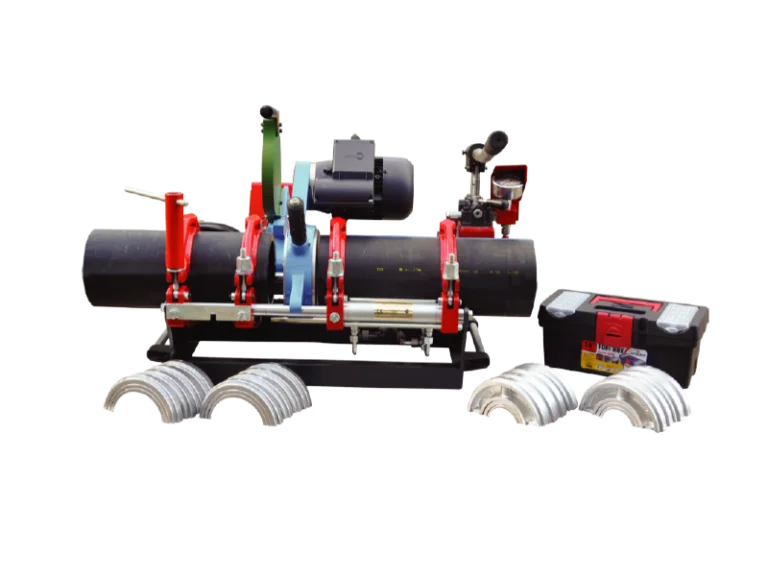
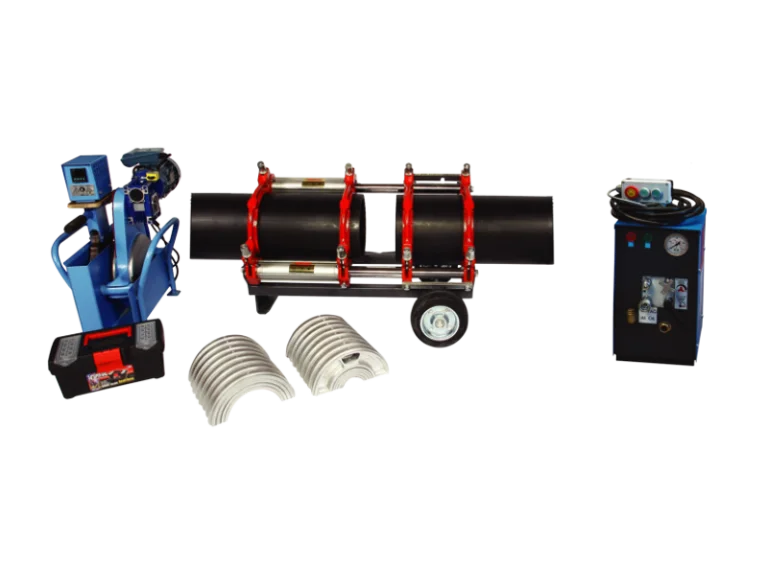
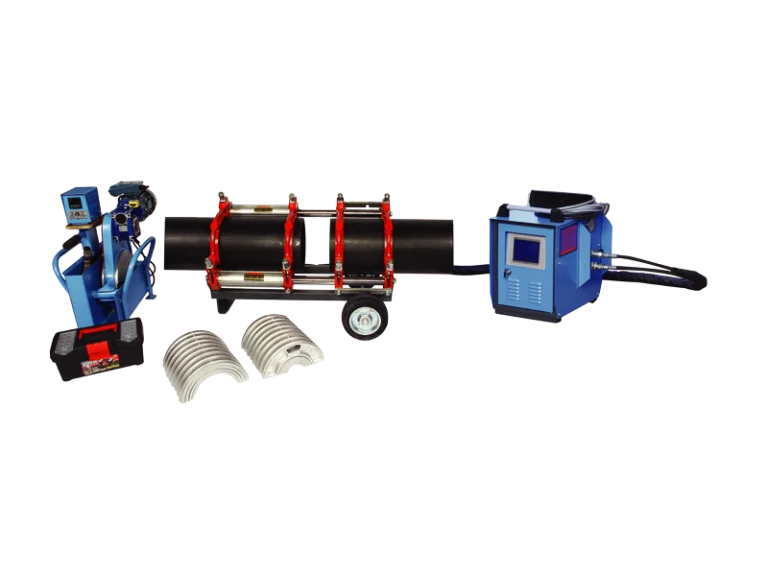
Butt Fusion Machine
Hydraulic and CNC butt fusion machines for PE and PP pipe, from compact site machines to Ø 1600 mm mains.
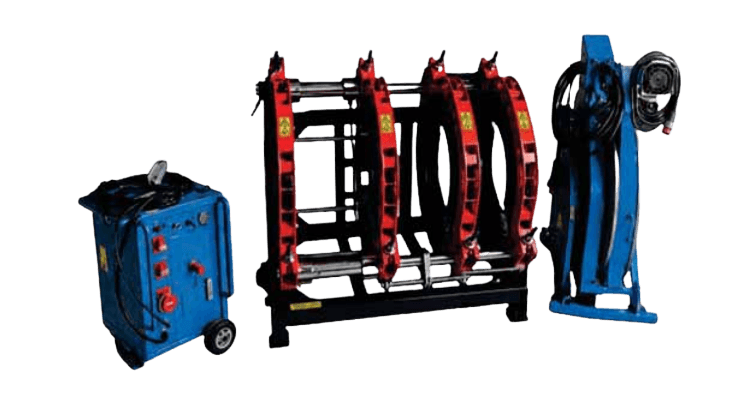
Weldable diameters
Technical Data
Welding Range
Ø 630 – Ø 1000 mm
Power Supply
380 V / 50 Hz, 3PH
Total Power
24.5 kW
Heater
17.5 kW
Trimmer
3 kW
Hydraulic Unit
4 kW
Pressure Adjusting Range
0 – 12 MPa
Max Temperature
270 °C
Material
PE, PP
Electric System
Triple phase
Packaging & Transport
Package 1 (gross / net)
1769 / 1767 kg
Package 1 dimension
210 × 120 × 200 cm
Package 2 (gross / net)
193 / 172 kg
Package 2 dimension
74 × 66 × 106 cm
Total packages
2
Total gross / net
1962 / 1939 kg
The ALW 1000A is a butt fusion machine for PE and PP pipe from Ø 630 to Ø 1000 mm. Power supply is 380 V / 50 Hz, 3PH. Total installed power is 24.5 kW. Welding pressures and times come from the DVS 2207 parameter table; the full procedure is under Technical Guides below. It belongs to the ALW A series, the newer generation of our AL platform with an updated hydraulic unit and refined controls.
- Place pieces in the clamps; insert the trimmer and face until 100% contact.
- Remove trimmer, insert heater (~220 ℃); push at 0.15 N/mm² to form the lip.
- Equalize temperature at almost zero pressure (0.01 N/mm²) with heater in place.
- Remove heater; join the pieces at 0.15 N/mm².
- Hold joining pressure for the required time, then release.
- Leave the joint to cool under the specified time.
| Wall (mm) | Lip (mm) | Heat (s) | Remove heater (s) | Fuse (s) | Cool (min) |
|---|---|---|---|---|---|
| up to 4.5 | 0.5 | 45 | 5 | 5 | 6 |
| 4.5–7 | 1 | 70 | 6 | 6 | 10 |
| 7–12 | 1.5 | 120 | 8 | 8 | 16 |
| 12–19 | 2 | 190 | 10 | 11 | 24 |
| 19–26 | 2.5 | 260 | 12 | 14 | 32 |
| 26–37 | 3 | 370 | 16 | 19 | 45 |
| 37–50 | 3.5 | 500 | 20 | 25 | 60 |
| 50–70 | 4 | 700 | 25 | 35 | 80 |
Visibility
Butt welds are visible and can be redone on the spot; EF welds hide inside the socket and need experienced welders.
Hard to reach places
EF wins: tiny machine, cable tip electrodes. Works above ground, in pits, anywhere.
Simplicity
Butt welding forgives workmanship errors; EF has zero tolerance and fails only at pressure test.
Material conditions
EF demands matching MFI, round pipes, clean surfaces, stable voltage; butt is unaffected by these.
Cost
Butt is far cheaper: no copper wire sockets every 6/12 m.
Strength
A correct butt weld is the strongest point of the line (the 'lip' adds wall thickness).
| Vehicle | L × W × H (m) | Volume | Max Load |
|---|---|---|---|
| 20 FT Container | 5.89 × 2.34 × 2.37 | 33 m³ | 24,850 kg |
| 40 FT Container | 11.90 × 2.34 × 2.38 | 67 m³ | 28,800 kg |
| 40 FT High Cube | 11.90 × 2.34 × 2.67 | 76 m³ | 30,200 kg |
| 45 FT High Cube | 13.00 × 2.34 × 2.67 | 86 m³ | 27,820 kg |
| Normal TIR | 13.6 × 2.45 | 100 m³ | — |
| Maxima TIR | 13.6 × 2.45 | 112 m³ | — |
| Jumbo TIR | 13.6 × 2.45 | 97 m³ | — |
| Truck + Trailer | 7.5 + 9.6 | 56 m³ | — |
Potable water lines, force mains, drainage and siphonic systems, natural gas distribution, agricultural irrigation and industrial pipelines. Fittings manufactured to TS EN 1555-3:2010+A1 • TS EN 12201-3+A1 • TS EN 15494 • CE; machines to TS ISO 12176-1 and DVS 2207 welding practice.
Catalogs, user manuals and training videos are available on request.
Request Documents