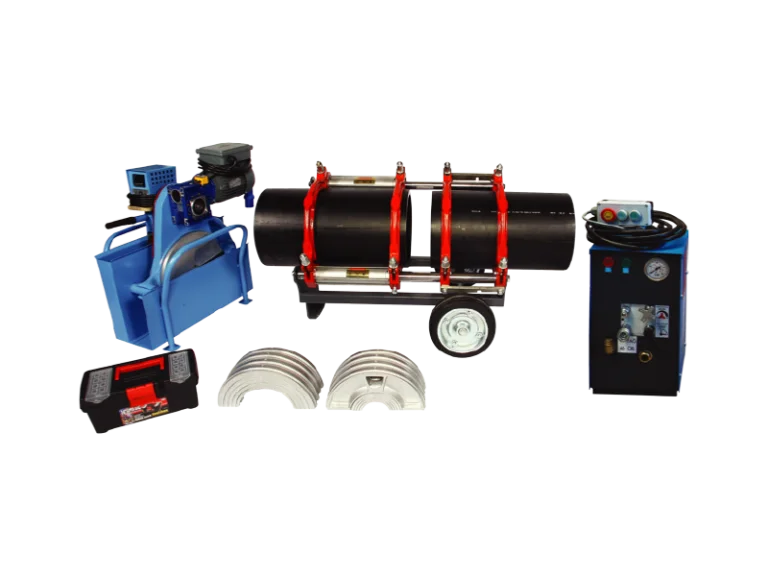
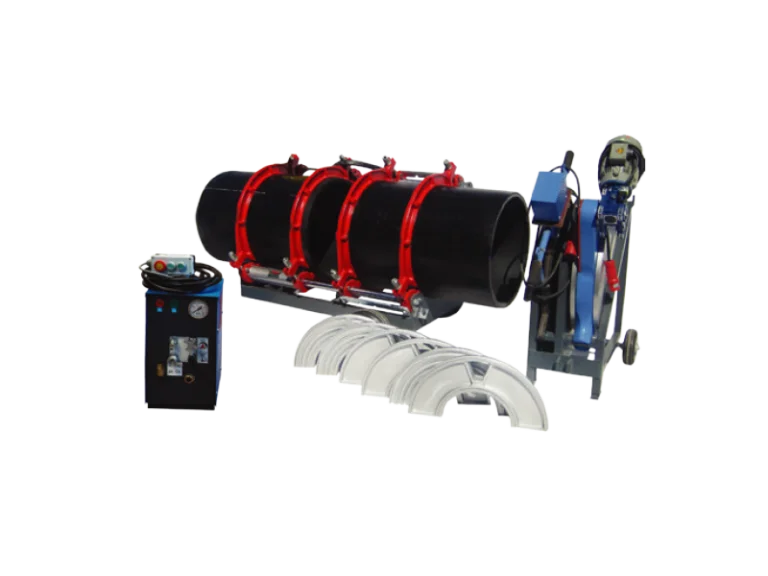
AL 630
Butt Fusion Machine
Hydraulic and CNC butt fusion machines for PE and PP pipe, from compact site machines to Ø 1600 mm mains.
Weldable diameters
Technical Data
Welding Range
Ø 315 – Ø 630 mm
Material
PE, PP
Max Wall Thickness
PN 32
Power Supply
380 V, Triple phase
Heater
7.5 kW
Trimmer
1.5 kW
Hydraulic Unit
0.75 kW
Total Power
9.75 kW
Operating Pressure
150 Bar
Required Generator
16 kVA
Electric System
Triple phase
Packaging & Transport
Package
2 wooden crates
Crate dimensions
123 × 162 × 134 cm; 75 × 122 × 149 cm
Net / Gross Weight
669 / 812 kg
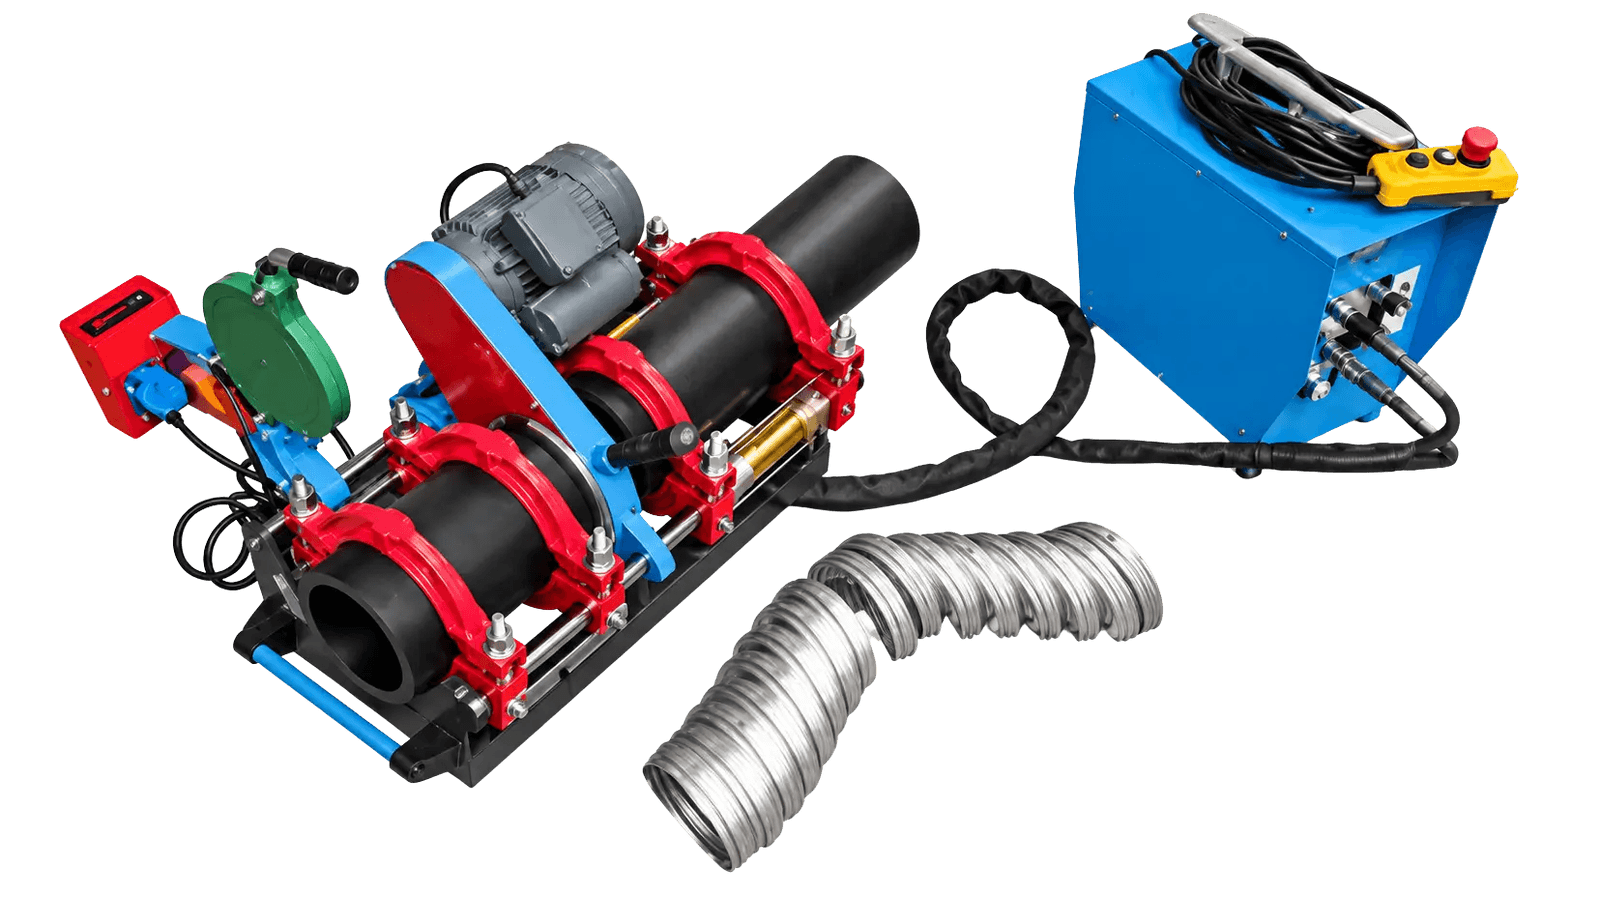
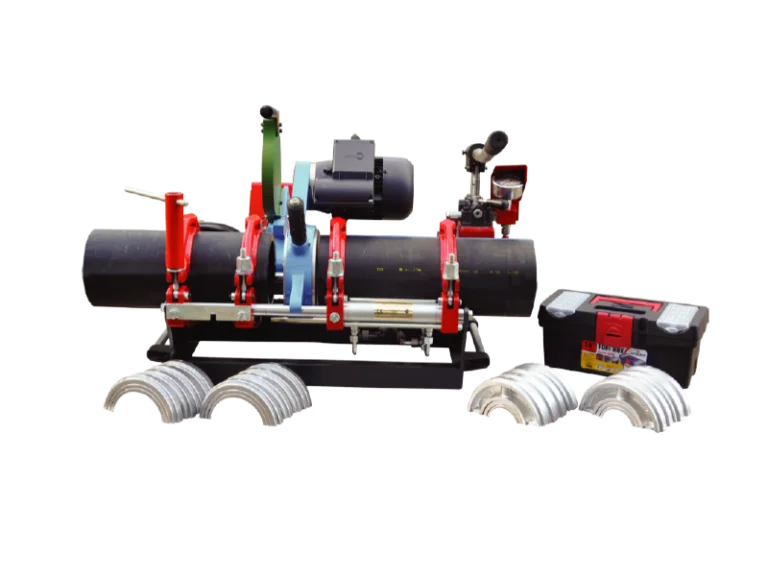
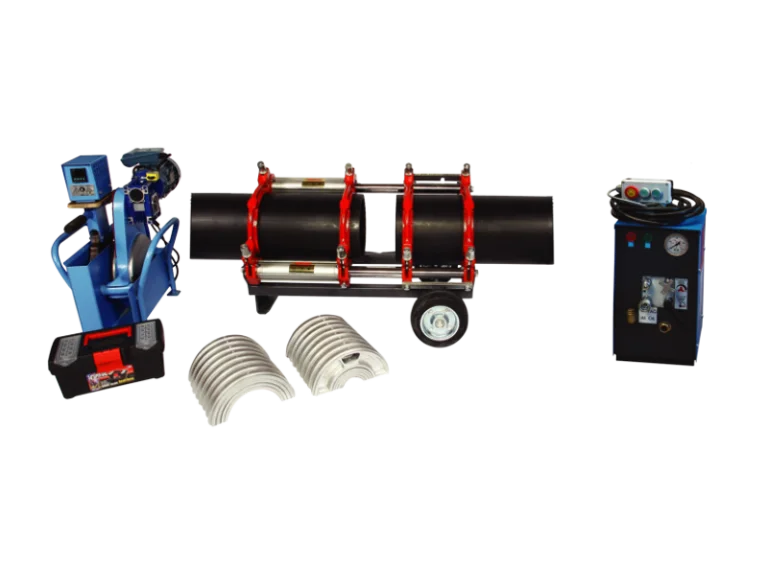
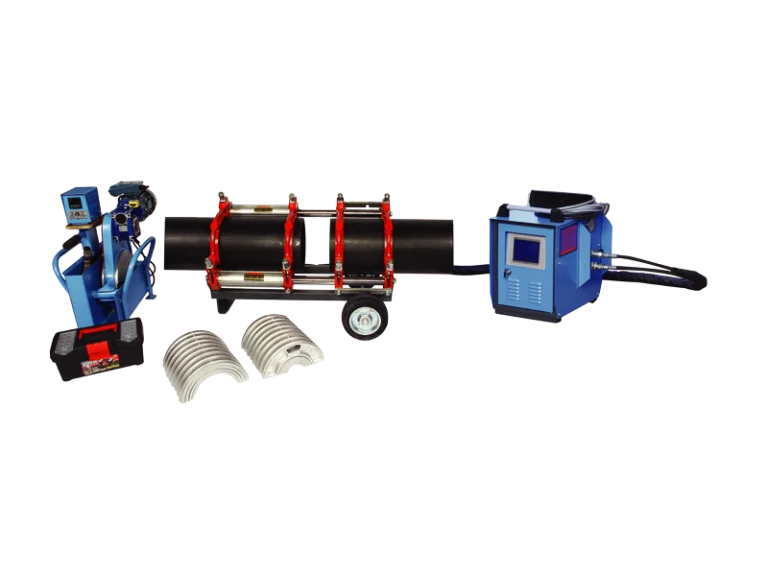
The AL 630 is a butt fusion machine for PE and PP pipe from Ø 315 to Ø 630 mm. It welds pipe walls up to PN 32. Power supply is 380 V, Triple phase. Total installed power is 9.75 kW. On site you will need a generator of at least 16 kVA. Welding pressures and times come from the DVS 2207 parameter table; the full procedure is under Technical Guides below. It ships in 2 wooden crates. Crate sizes and weights are listed under Packaging & Transport.
- Place pieces in the clamps; insert the trimmer and face until 100% contact.
- Remove trimmer, insert heater (~220 ℃); push at 0.15 N/mm² to form the lip.
- Equalize temperature at almost zero pressure (0.01 N/mm²) with heater in place.
- Remove heater; join the pieces at 0.15 N/mm².
- Hold joining pressure for the required time, then release.
- Leave the joint to cool under the specified time.
| Wall (mm) | Lip (mm) | Heat (s) | Remove heater (s) | Fuse (s) | Cool (min) |
|---|---|---|---|---|---|
| up to 4.5 | 0.5 | 45 | 5 | 5 | 6 |
| 4.5–7 | 1 | 70 | 6 | 6 | 10 |
| 7–12 | 1.5 | 120 | 8 | 8 | 16 |
| 12–19 | 2 | 190 | 10 | 11 | 24 |
| 19–26 | 2.5 | 260 | 12 | 14 | 32 |
| 26–37 | 3 | 370 | 16 | 19 | 45 |
| 37–50 | 3.5 | 500 | 20 | 25 | 60 |
| 50–70 | 4 | 700 | 25 | 35 | 80 |
Visibility
Butt welds are visible and can be redone on the spot; EF welds hide inside the socket and need experienced welders.
Hard to reach places
EF wins: tiny machine, cable tip electrodes. Works above ground, in pits, anywhere.
Simplicity
Butt welding forgives workmanship errors; EF has zero tolerance and fails only at pressure test.
Material conditions
EF demands matching MFI, round pipes, clean surfaces, stable voltage; butt is unaffected by these.
Cost
Butt is far cheaper: no copper wire sockets every 6/12 m.
Strength
A correct butt weld is the strongest point of the line (the 'lip' adds wall thickness).
| Vehicle | L × W × H (m) | Volume | Max Load |
|---|---|---|---|
| 20 FT Container | 5.89 × 2.34 × 2.37 | 33 m³ | 24,850 kg |
| 40 FT Container | 11.90 × 2.34 × 2.38 | 67 m³ | 28,800 kg |
| 40 FT High Cube | 11.90 × 2.34 × 2.67 | 76 m³ | 30,200 kg |
| 45 FT High Cube | 13.00 × 2.34 × 2.67 | 86 m³ | 27,820 kg |
| Normal TIR | 13.6 × 2.45 | 100 m³ | — |
| Maxima TIR | 13.6 × 2.45 | 112 m³ | — |
| Jumbo TIR | 13.6 × 2.45 | 97 m³ | — |
| Truck + Trailer | 7.5 + 9.6 | 56 m³ | — |
Potable water lines, force mains, drainage and siphonic systems, natural gas distribution, agricultural irrigation and industrial pipelines. Fittings manufactured to TS EN 1555-3:2010+A1 • TS EN 12201-3+A1 • TS EN 15494 • CE; machines to TS ISO 12176-1 and DVS 2207 welding practice.
Catalogs, user manuals and training videos are available on request.
Request Documents